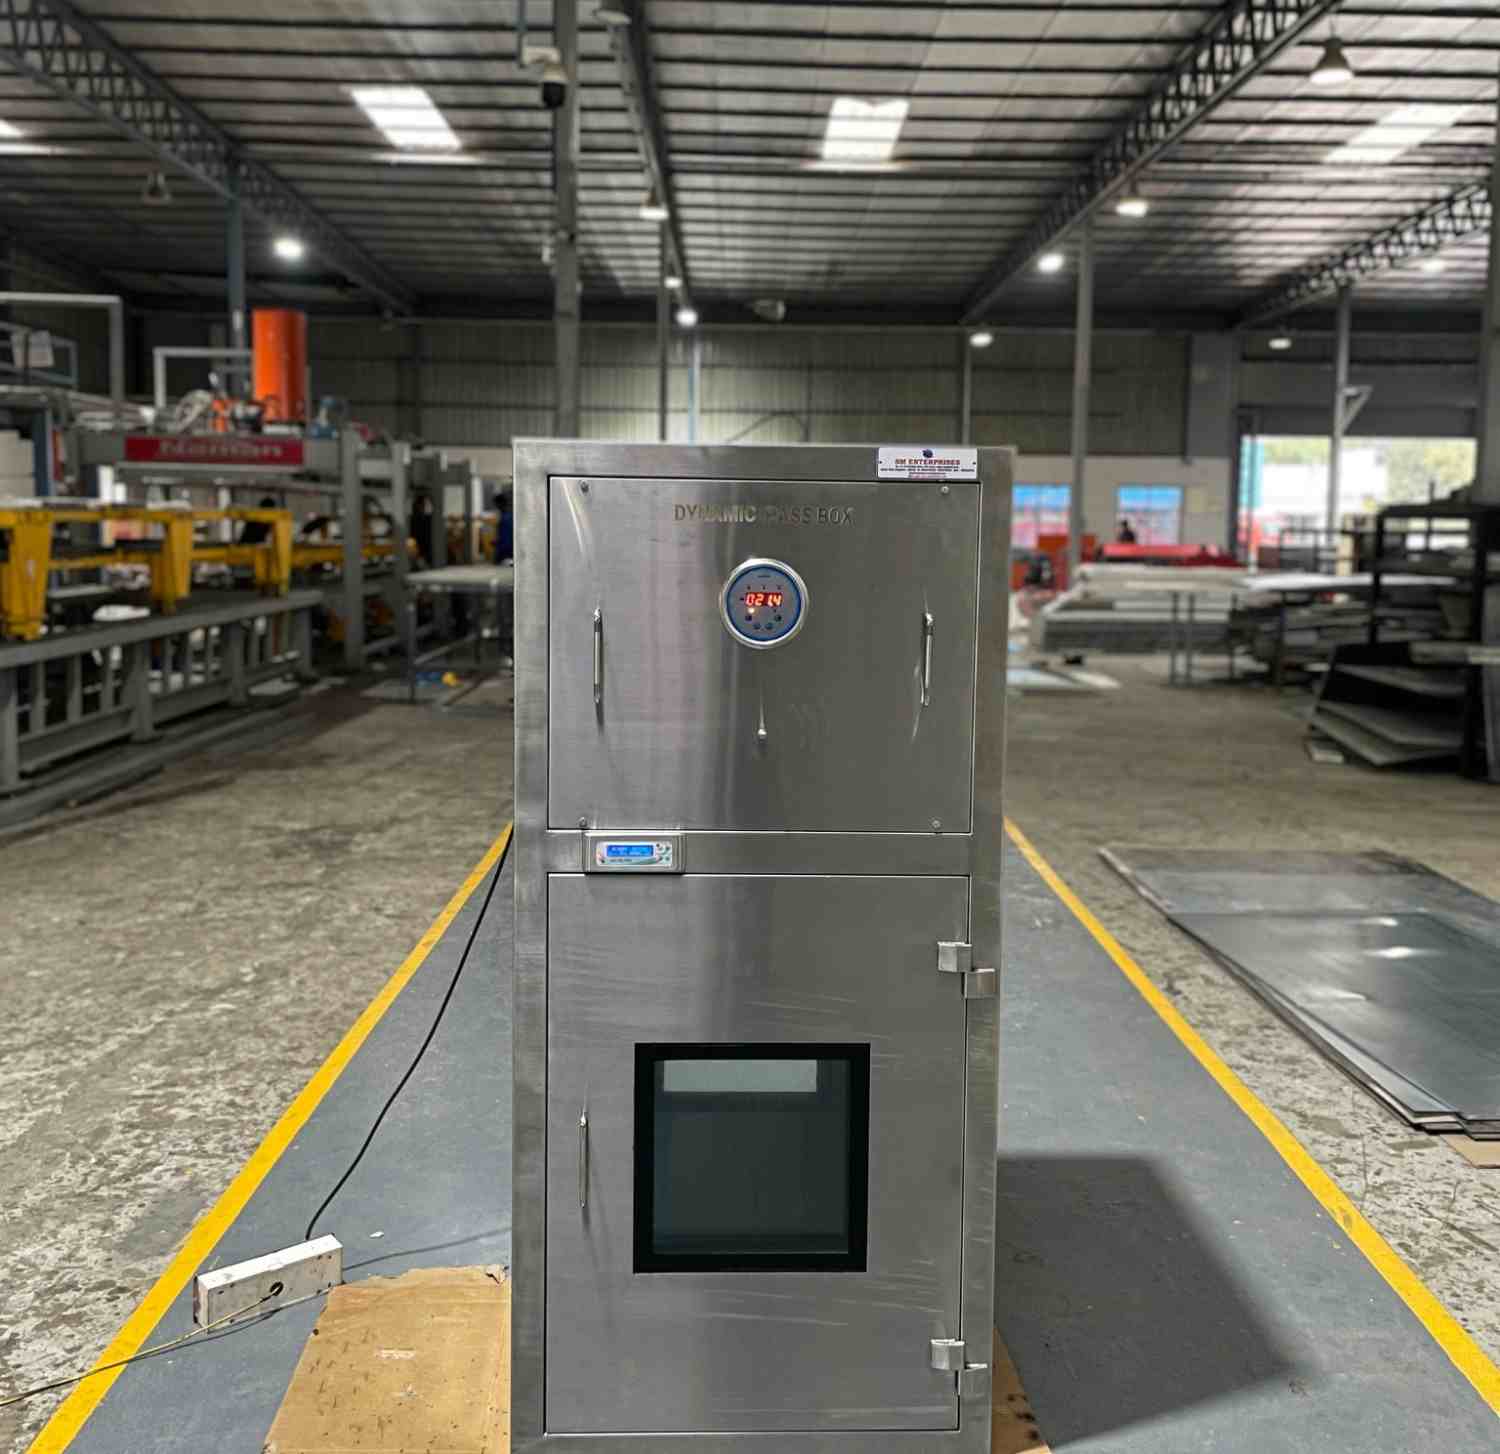

Customized Modular Cleanroom Solutions help industries establish controlled environments according to their specific operational requirements. Pharmaceutical manufacturing units, healthcare facilities, biotechnology laboratories, and electronics industries benefit from properly designed cleanroom infrastructure. These systems include prefabricated wall panels, ceiling panels, modular partitions, riser panels, and specialized accessories. Different PPGI and PCGI finishes, along with PUF and Rockwool infill options, provide flexibility in material selection. Proper layout planning and coordinated installation support efficient space utilization, hygiene, and contamination control. Modular construction also allows businesses to accommodate changing facility requirements, maintenance activities, and future expansion.